Case Study: Custom EVA Hard Shell Case for Medical
author: Tony
2022-11-08

Client Background:
Dingfeng Bag Factory is a leading manufacturer specializing in the production of custom bags and cases. They were approached by a medical equipment company to develop a custom EVA hard shell case for their sensitive medical devices. The client required a durable and protective solution to safely transport and store their equipment while ensuring ease of use and convenient organization.
Dingfeng Bag Factory is a leading manufacturer specializing in the production of custom bags and cases. They were approached by a medical equipment company to develop a custom EVA hard shell case for their sensitive medical devices. The client required a durable and protective solution to safely transport and store their equipment while ensuring ease of use and convenient organization.
Client Goals:
Provide a customized solution that meets the specific requirements of their medical equipment.
Ensure the highest level of protection for sensitive devices during transportation and storage.
Enhance the usability and convenience of the case for medical professionals.
Strengthen the client's brand image through a high-quality and professional-looking case.
Challenges:
Understanding the precise dimensions, shapes, and sensitivities of the medical equipment.
Designing a custom case that offers optimal protection while maintaining a compact and portable form factor.
Selecting appropriate materials to ensure impact resistance, water resistance, and durability.
Collaborating closely with the client to incorporate their branding elements and meet their specifications.
Strategy and Execution:
Requirement Gathering:
Conducted extensive discussions with the client to understand the specific requirements and sensitivities of their medical equipment.
Identified the dimensions, shapes, and fragility of the devices that needed to be accommodated within the case.
Assessed the client's branding requirements and preferences.
Design and Prototyping:
Developed initial concepts and designs for the custom EVA hard shell case.
Utilized computer-aided design (CAD) software to create detailed 3D models.
Produced physical prototypes to evaluate the fit, protection, and usability of the case.
Developed initial concepts and designs for the custom EVA hard shell case.
Utilized computer-aided design (CAD) software to create detailed 3D models.
Produced physical prototypes to evaluate the fit, protection, and usability of the case.
Material Selection and Construction:
Selected high-quality EVA (ethylene-vinyl acetate) material known for its impact resistance and durability.
Evaluated different foam types and densities to create custom inserts that securely hold the medical devices in place.
Designed the case with additional features like compartments, straps, and handles to enhance usability and convenience.
Branding and Customization:
Incorporated the client's branding elements, such as logos and color schemes, into the design of the case.
Utilized custom printing, embroidery, or labeling techniques to prominently display the client's brand on the case.
Ensured the overall aesthetics of the case aligned with the client's professional image.
Quality Assurance:
Conducted rigorous quality checks during the manufacturing process to ensure the case met the desired standards.
Tested the case for impact resistance, water resistance, and overall protection.
Ensured that the case complied with relevant industry regulations and certifications.
Conducted rigorous quality checks during the manufacturing process to ensure the case met the desired standards.
Tested the case for impact resistance, water resistance, and overall protection.
Ensured that the case complied with relevant industry regulations and certifications.
Results:
Customized Solution:
Dingfeng Bag Factory successfully developed a custom EVA hard shell case that precisely fit the client's medical equipment.
The case provided optimal protection, preventing damage during transportation and storage.
The case provided optimal protection, preventing damage during transportation and storage.
Enhanced Protection and Usability:
The case's foam inserts securely held the sensitive devices in place, minimizing the risk of impact or movement.
Additional features such as compartments, straps, and handles allowed for easy organization and transportation of the equipment.
Additional features such as compartments, straps, and handles allowed for easy organization and transportation of the equipment.
Strengthened Brand Image:
The custom branding elements prominently displayed on the case enhanced the client's brand visibility and professionalism.
The high-quality and professional-looking case positively influenced the perception of the client's medical equipment.
The custom branding elements prominently displayed on the case enhanced the client's brand visibility and professionalism.
The high-quality and professional-looking case positively influenced the perception of the client's medical equipment.
Customer Satisfaction and Repeat Business:
The custom EVA hard shell case met the client's expectations and requirements, resulting in a high level of customer satisfaction.
The client expressed their intention to continue working with Dingfeng Bag Factory for future projects, leading to a potential long-term partnership.
The custom EVA hard shell case met the client's expectations and requirements, resulting in a high level of customer satisfaction.
The client expressed their intention to continue working with Dingfeng Bag Factory for future projects, leading to a potential long-term partnership.
Competitive Advantage:
The custom EVA hard shell case provided the client with a unique and customized solution for their medical equipment.
This gave the client a competitive edge by offering a superior level of protection and convenience compared to off-the-shelf cases.
The custom EVA hard shell case provided the client with a unique and customized solution for their medical equipment.
This gave the client a competitive edge by offering a superior level of protection and convenience compared to off-the-shelf cases.
Cost-Effective Manufacturing:
Dingfeng Bag Factory optimized the manufacturing process to ensure cost-effectiveness without compromising quality.
Efficient production methods and material sourcing helped keep the overall manufacturing costs within the client's budget.
Dingfeng Bag Factory optimized the manufacturing process to ensure cost-effectiveness without compromising quality.
Efficient production methods and material sourcing helped keep the overall manufacturing costs within the client's budget.
How Dingfeng can produce bags with low price and high quality
OEM Manufacturing Outdoor Camping Bags
Related Article
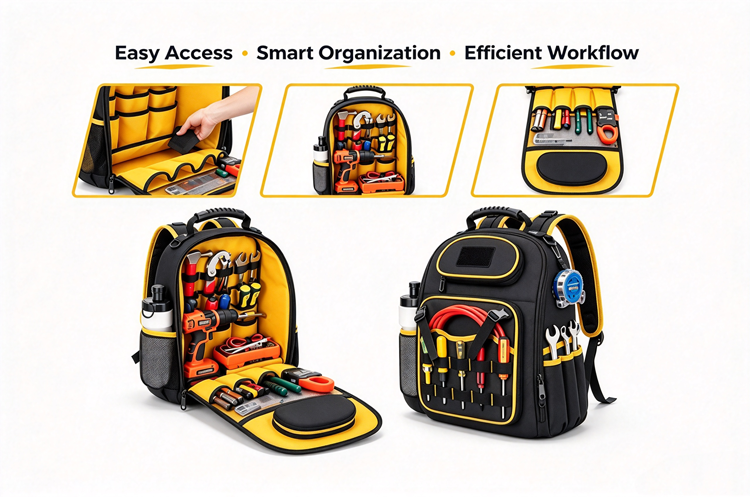
This article explores how accessibility, organization, and workflow can improve equipment bag design. Learn how thoughtful pocket layouts, custom compartments, and practical storage features help users keep tools and equipment organized, access essentials quickly, and work more efficiently.
The Future of Equipment Storage: Accessibility, Organization, and Workflow
Get ahead on your 2027 product plans. Understand the custom bag development process and how early preparation helps keep your project on track.
Planning Ahead for 2027: Starting Your Custom Bag Development Early
China's Mid-Autumn Festival and Golden Week create a tight production window for Q4 orders. Discover why custom bag lead times can extend beyond standard production schedules, how to plan backward from your delivery date, and why fall is a good time to start developing your 2027 products.
Mid-Autumn & Golden Week 2026: The Manufacturing Reality Behind Q4 Delivery Dates

This article explores how custom lid organizers and padded divider systems can transform unused hard case space into practical, high-value storage. By improving organization, accessibility, protection, and workflow efficiency, these interior solutions enhance the user experience while helping brands create more premium, versatile, and marketable hard case products.
Maximizing Hard Case Storage: How Lid Organizers and Divider Systems Turn Dead Space into Value